Get in touch with UDTECH Company

UD Machine Solution Technology Co., Ltd. | Automation in food production since 2003
How an automatic egg roll machine works depends on its product class: buyer search terms for batter-fed wafer equipment include “automatic egg roll making machine” and “fully automatic egg roll roller machine”; this class measures batter, bakes a thin sheet, releases it while bendable, optionally adds filling or a core, rolls it, and conveys it to cooling and collection. How an automatic egg roll machine works is a timed sequence. It coordinates batter metering, baking, optional core injection, rolling, cooling, and transfer. Finished-roll quality results from several synchronized transitions rather than a single temperature or speed.
That distinction is relevant. A prepared-sheet spring roll or savory egg roll line uses a dough belt, adds filling, folds, seals, and rolls before frying; this is a different machine class. This guide focuses on the batter-fed baked-wafer class sold for crisp egg rolls, wafer rolls, and similar forms. Whereas this guide compares the two forming classes, a poor purchasing choice or a high-quality output that isn’t justified will result.
Short answer
In operation, the machine converts a recipe into a timed, repetitive cycle. Batter conditioning and metering, heat, dwell, transfer, rolling, and more must fall in a controlled range. Good output forms and moves forward only when batter and sheet forming, heat, dwell, transfer, and rolling conditions stay within a specified range.
How a Wafer-Style Automatic Egg Roll Machine Works in One Cycle
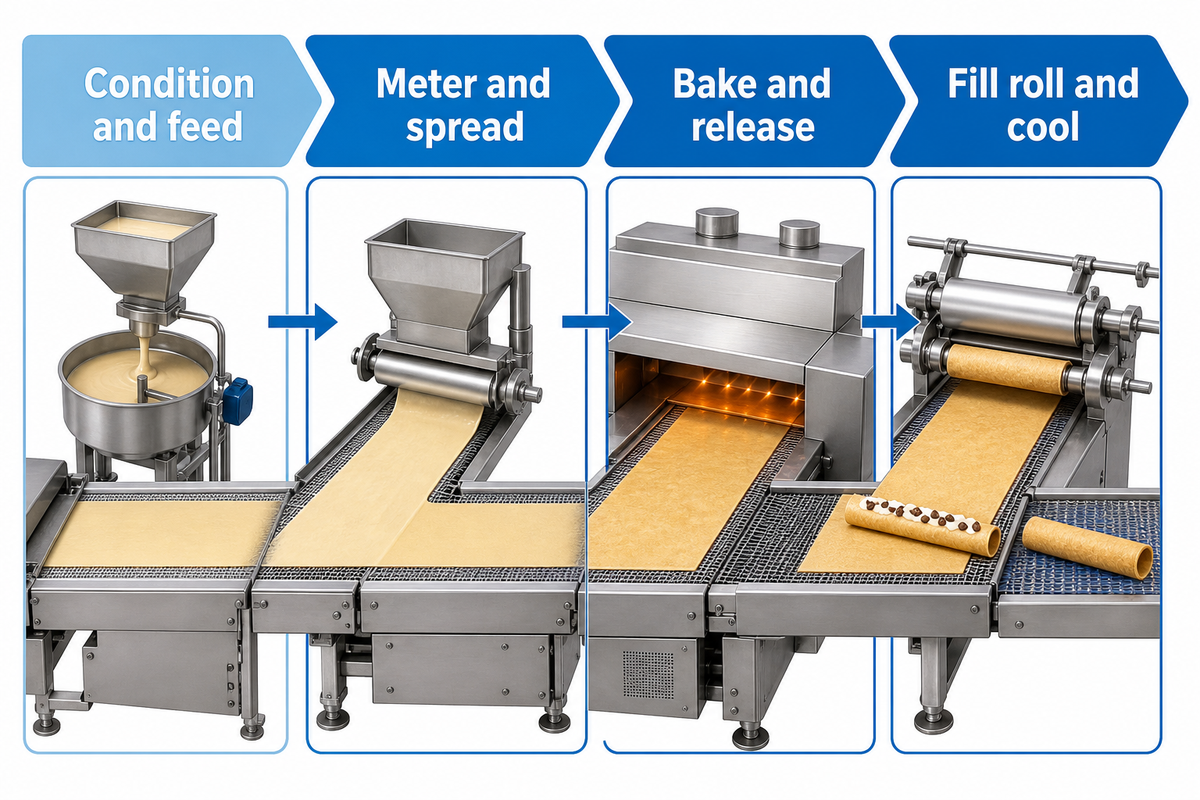
Physically, the task is simple and straightforward to describe. For automated food production, a full automatic egg roll machine creates a thin baked sheet and forms it before it hardens while repeating the timed cycle under stable, repeatable process conditions.
- Condition and feed the batter. Mixing and holding should help achieve consistency for repeated dosing.
- Meter each deposit. The dosing system delivers the mass needed for the target sheet size and thickness.
- Spread or close the baking surfaces. Machine geometry converts the deposit into a controlled thin layer.
- Bake the sheet. Heat and dwell remove water, develop color, and establish release behavior.
- Release and transfer. The sheet leaves the surface intact and reaches the next station before it loses too much flexibility.
- Fill and roll when specified. A depositor, mandrel or rolling tool creates the required core and geometry.
- Cool, inspect, and discharge. The roll sets and moves away from the forming region towards collection or packaging.
UD’s automatic egg roll machine specifications specify that the system is production dependent and comprises batter spreading, baking, core injection, rolling, and downstream systems. Note that these specifications are first-party configuration statements. They indicate to the customer what needs to be validated. They don’t ensure that each recipe/installation is the same.
Older patents set class limits. One of the patent applications claims baking a flowable dough into a still-deformable strip and sending it to a winding instrument. Another claim for an “automatic egg roll machine” states that it begins with a prepared sheet, and fills, seals, and rolls it. Just because the machine is “automatic” doesn’t mean the materials path is the same.
Start With Batter Condition and Metered Dosing
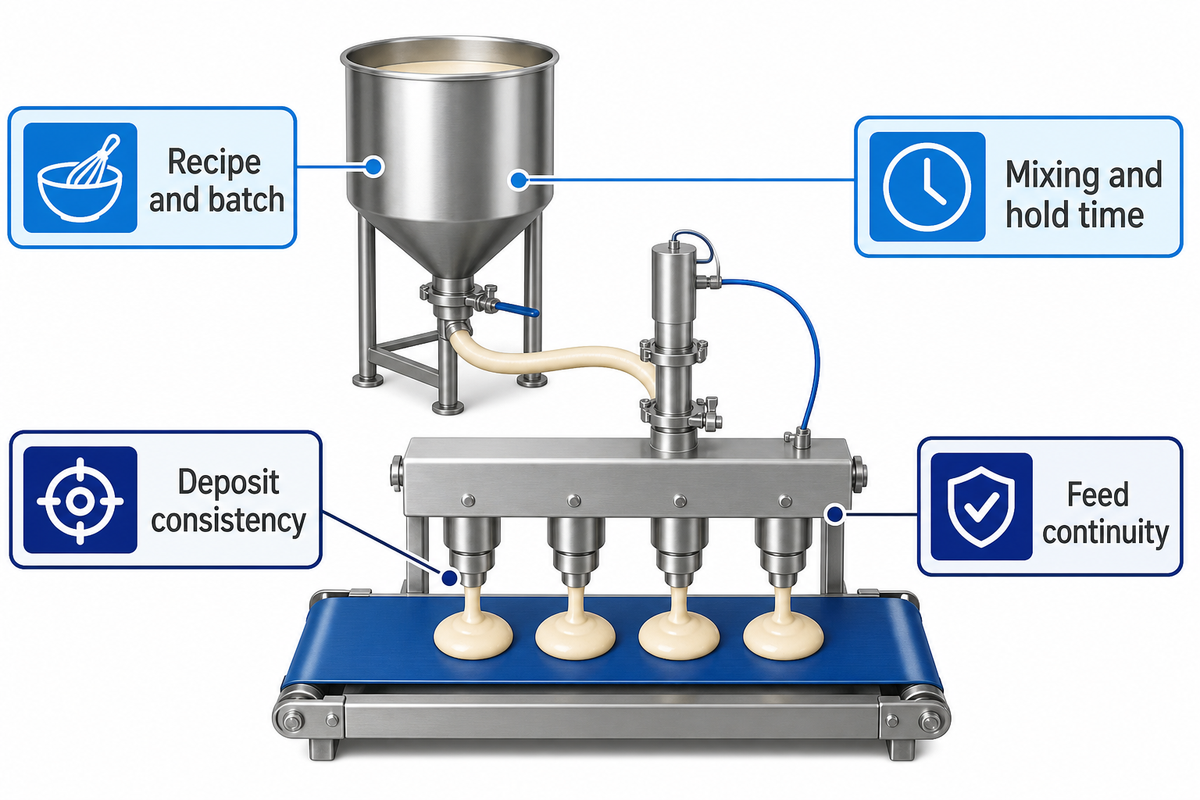
Sheet defects can begin before the baking surface. If solids settle in a holding tank, the mixture warms, or feed pressure changes, then equal timing will no longer guarantee equal deposits. A useful first operating record isn’t “heater on.” It’s recipe identity, mixing sequence, batter age, batter temperature, observed flow, and mass of deposit.
| Record | Why it matters | Practical check |
|---|---|---|
| Recipe and batch | Separates machine drift from ingredient drift | Use one identified batch during comparison runs |
| Mixing and hold time | Changes hydration, aeration, and feed behavior | Timestamp mixing end and first deposit |
| Deposit consistency | Drives sheet mass and geometry | Weigh a short sequence before tuning heat |
| Feed continuity | Air, pulsing, or level changes disturb dosing | Observe start, steady run, and low-level behavior |
The machine can’t handle all recipe changes by adding heat. Independent waffle research found that changing starch, sugar and humectant choices altered sticking, take-off force, baking loss, and product stability in the research conditions. The main lesson of this research isn’t the study recipe, but rather the interaction. The formulation and machine settings must be validated together.
How the Machine Forms a Repeatable Wafer Sheet
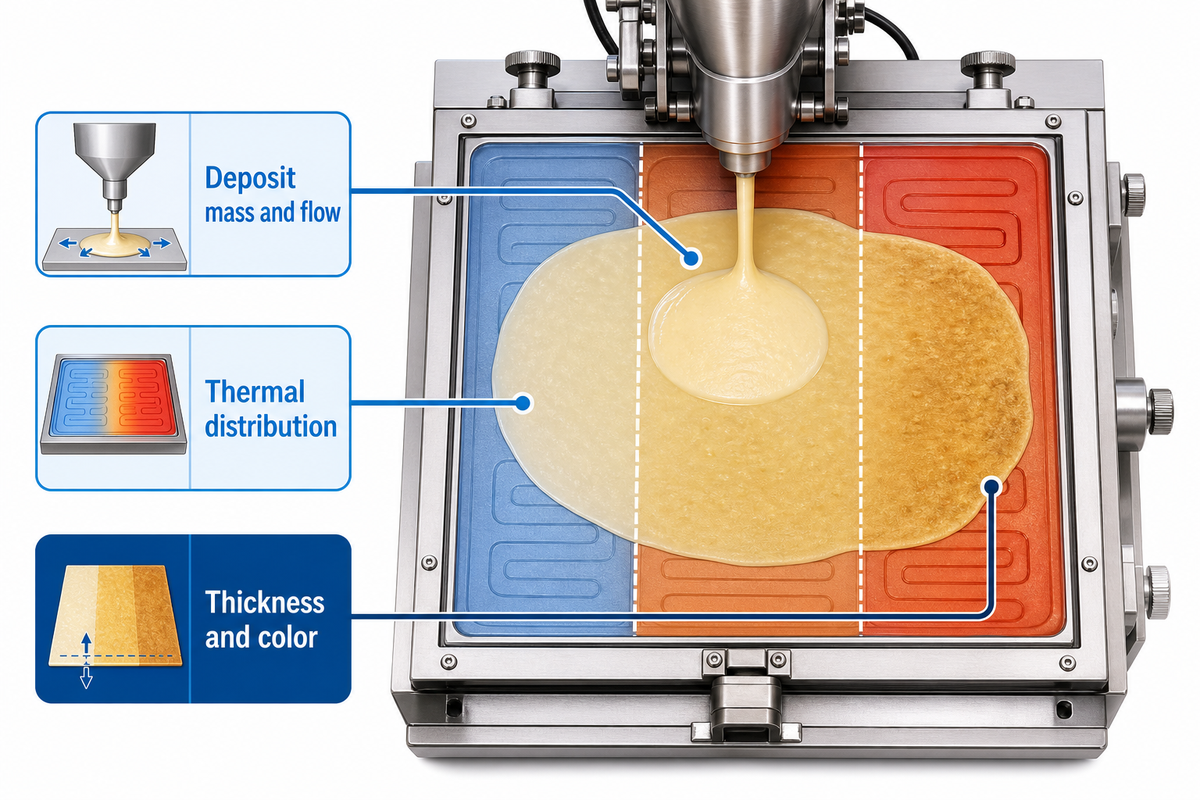
Once a deposit reaches the forming area, the spreading geometry, condition of the surface, plate closure, and distribution of heat define the sheet. Thickness isn’t simply a gap setting. Deposit mass and flow dictate how much material is required to occupy that gap, while temperature and dwell dictate how the sheet dries and releases.
One published study of industrial batch waffle baking in 2025 examined baking plates, measured thermal distribution, sheet thickness, and color. In this study, changing the plates affected how uniformly heat was distributed, the stability of the thickness and color, respectively. This is a useful starting point for troubleshooting: two zones can show similar setpoints, but transfer heat differently depending on what’s on the surface, how worn the plates are, or what’s directly below the sensor.
The article also outlines performance figures, but they aren’t standard machine settings. The sheet thickness, production rate, batter composition, and measured temperatures pertain to the tested line. The supplier should conduct trials for the requested diameter, wall thickness, color band, and release behavior on the buyer’s sample and envisioned energy source.
| Source | Published context | Safe use |
|---|---|---|
| 2025 wafer-plate study | The article’s background cites 52–60% water and about 150–180 °C; its experiment tested 23 and 31 pieces/min of wafer sheets against a stated acceptable band of 2.8–3.2 mm | Keep cited background ranges and the acceptable band separate from measured results, which extended to 2.78–3.19 mm |
| 2017 experimental waffle study | The article’s background cites 140–180 °C and 110–180 seconds; one rice-flour treatment reported 46.7% sticking with very large dispersion (±50.7) | Formulation-specific evidence only, not an egg-roll recipe, industry rate, or acceptance limit |
| UD product page | 330 pieces/min for UD05-3; the shared family table publishes 0.8–1.4 mm wall thickness | Attributed first-party claims with model and family scope preserved; verify both in a witnessed run |
The 5-Variable Bake-and-Roll Control Window
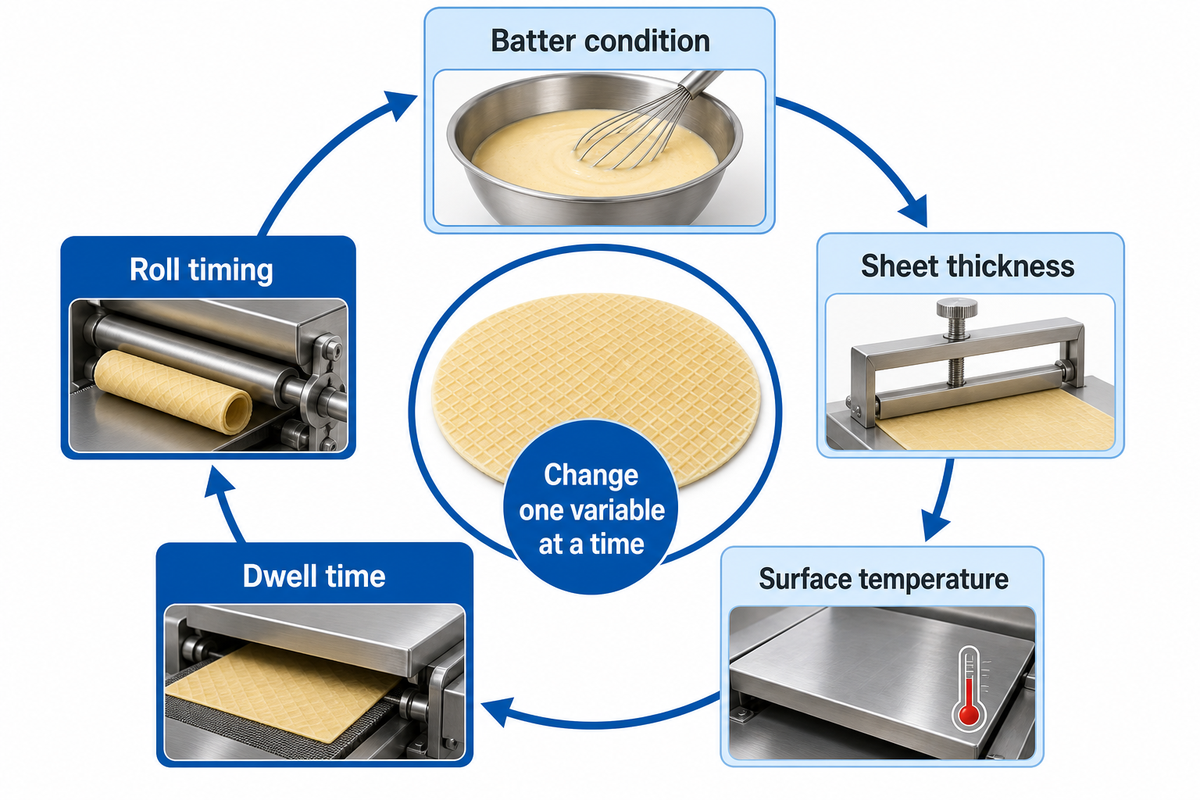
A dependable setup considers five in-machine variables as a single control window. Because often one variable must be moved to change another, operators should change one variable at a time and record the result.
| Variable | If it drifts | Evidence to record |
|---|---|---|
| 1. Batter condition | Deposit and release behavior can change | Batch, age, temperature, and deposit mass |
| 2. Sheet thickness | Drying, flexibility, diameter, and bite change together | Measured sheet or wall thickness at several positions |
| 3. Surface temperature | Color and water removal become uneven | Zone readings plus product color observations |
| 4. Dwell time | The sheet can leave too soft or too brittle | Actual cycle time under steady load |
| 5. Roll timing | A released sheet can cool before it forms | Release-to-contact interval and crack count |
How do you produce well-formed egg rolls with automation?
Start with a standardized recipe and deposit, and then define sheet geometry before aiming for maximum speed. Bring the line to a declared warm state, record the five variables, check a timed sample, and adjust one variable at a time if the product fails to meet specifications.
Dark color is no indication of adequate moisture content, and a stable roll upon discharge won’t necessarily be stable after cooling. Check the first sample against agreed diameter, seam or overlap, breakage, and filling position. Repeat measurements after the planned run instead of basing the results on one visually attractive sample. Condition another sample for the agreed time, record the dispenser and temperature control settings, and verify whether a golden brown sample reaches the specified crisp texture; treat “crispy” as a measured result when teams produce egg rolls. If there’s a shift in the result due to cooling or exposure to the environment, consider that a finding within the boundaries of the process: the window in-machine may be stable, while the cooling or packaging processes may be unstable.
The post-bake boundary
The five-variable window ends at rolling. Cooling conditions, ambient relative humidity, moisture pickup, and packaging affect texture and mechanical behavior. There’s published research on low-moisture foods that links wafer texture and mechanics to moisture content, and this should be documented when a trial is designed to estimate the performance of the packaged shelf.
Transfer, Optional Filling, Rolling, and the Hidden Bottleneck
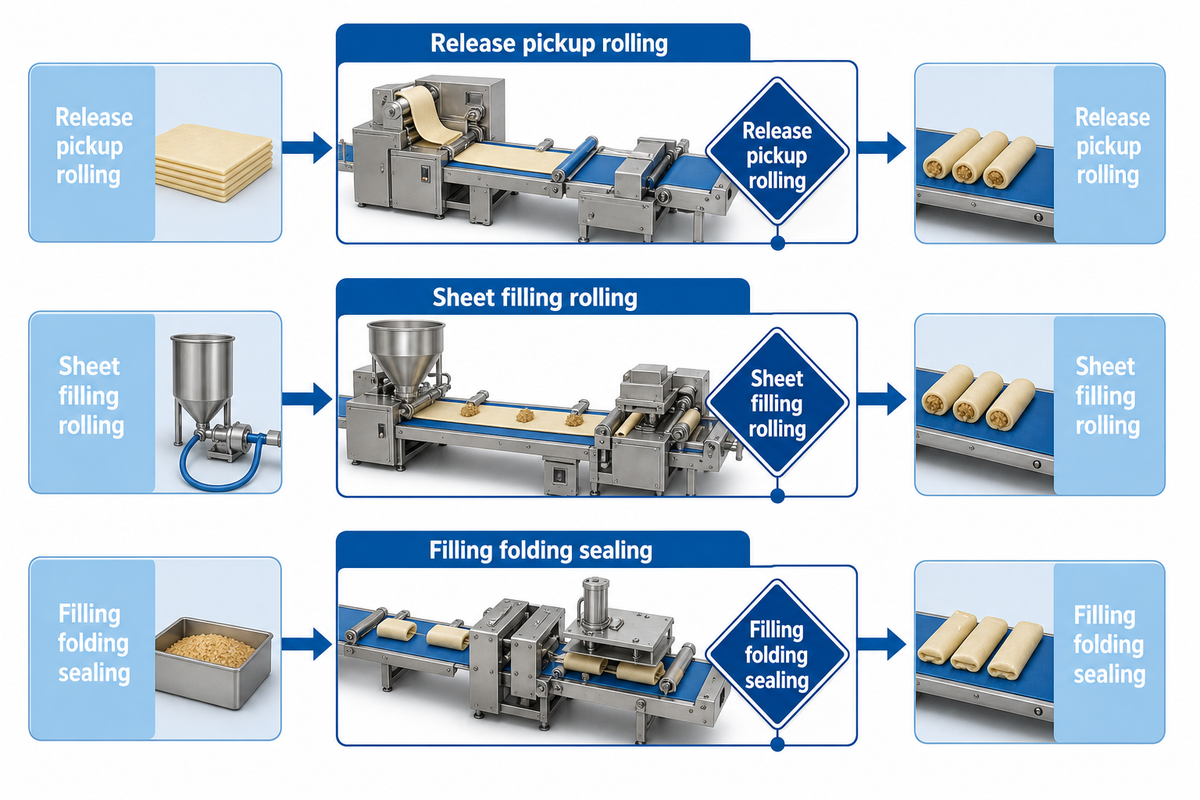
The sheet is most vulnerable when one station has finished its work and the following station hasn’t yet begun its work. On a baked-wafer line, a late pickup can result in cooling and cracking. Early or jagged pickup may lead to tearing or distortion of the sheet. The rolling tool must grip the sheet and shape it without plowing the surface, leaving a recessed or displaced core.
| Machine class | Sensitive handoff | Observed consequence | Witness check |
|---|---|---|---|
| Batter-fed baked wafer | Release → pickup → rolling | Sticking, tearing, cooling, or cracks | Film the handoff and count defects by station |
| Filled wafer roll | Sheet arrival → filling → rolling | Off-center core, leakage, or loose roll | Cut a timed sample and measure core position |
| Prepared-sheet filled roll | Filling → folding → sealing → rolling | Stretching, tearing, poor seal, or shape drift | Check sheet strength, dose placement, folds, and seal |
The hidden bottleneck is specific to each machine class. In the case of faster baking times, no benefit would be achieved if a hot wafer reached the roller outside the workable range. The same wouldn’t be true for a prepared-sheet line with no baked-sheet release where filling, folding support, sealing, or a dough’s tensile behavior may limit throughput.
What changes for plain, filled, wafer-stick, and phoenix-tail rolls?
Plain rolls may be void of filling. Filled rolls add depositor timing, core position, and leakage control. Wafer sticks can change mandrel diameter and cut length, while phoenix-tail products may require a different forming path. Review the phoenix roll machine options separately, then send the supplier the target dimensions, the filling condition, wall thickness, and the required texture.
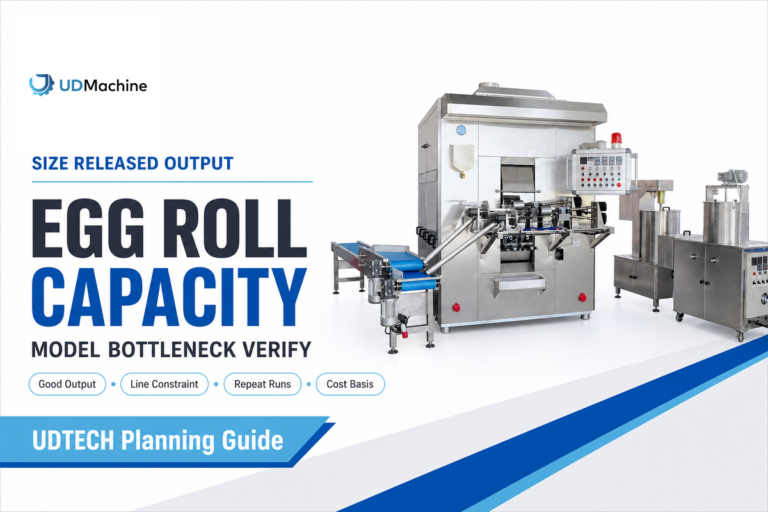
Why Nameplate Speed Is Not Yet Released Output
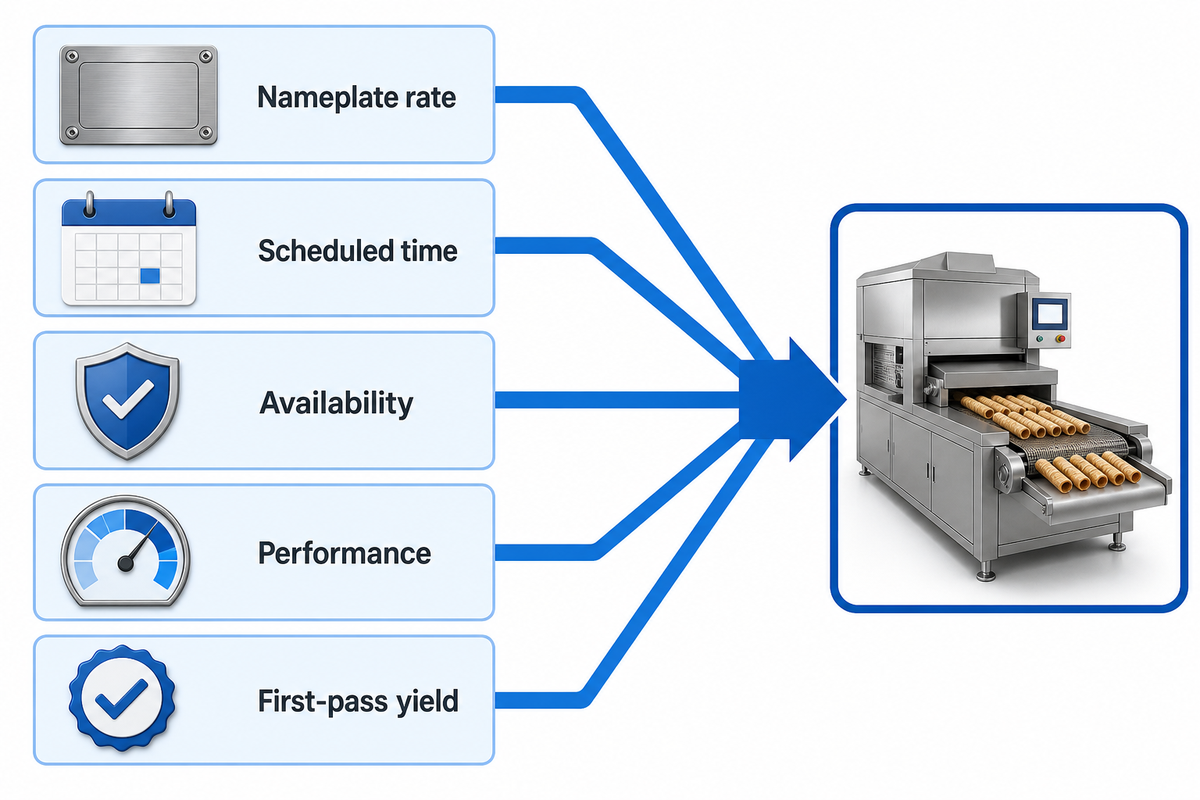
Nameplate speed is a valid reference point. Under the ideal condition described, nameplate speed is a reasonable expectation of good output. It can’t, however, define the number of good pieces a buyer will authorize in a production run. This would be a combination of the rate, speed loss while running, downtime, and defects.
Released-good output = nameplate rate × scheduled time × availability × performance × first-pass yield.
Availability discounts stops. Performance discounts slower running and minor interruptions while the machine is technically operating. First-pass yield discounts pieces that miss the agreed specification without rework. The University of Tennessee manufacturing-extension guide treats availability, performance, and quality as distinct measures, which prevents a common spreadsheet error: hiding speed loss inside uptime.
| Input | Example | Where the buyer gets it |
|---|---|---|
| Nameplate rate | 1,000 pieces/hour | Quoted model and product specification |
| Scheduled time | 1 hour | Trial plan |
| Availability | 90% | Stop log |
| Performance | 92% | Actual count versus ideal running count |
| First-pass yield | 96% | Accepted count divided by total count |
| Estimated good output | 795 pieces | 1,000 × 1 × 0.90 × 0.92 × 0.96 |
Each percent in the preceding examples is the output of a model. Please replace them with case specific values. This helps Finance compare labor costs per 1,000 good pieces and egg rolls per hour, lets Plant Management test high-volume production capacity and production efficiency, and allows Procurement to check whether the quoted configuration reduces labor costs. For deeper sizing, please check UD’s manual on egg roll machine capacity planning.
The 7-Symptom Process-Variable Diagnostic Grid
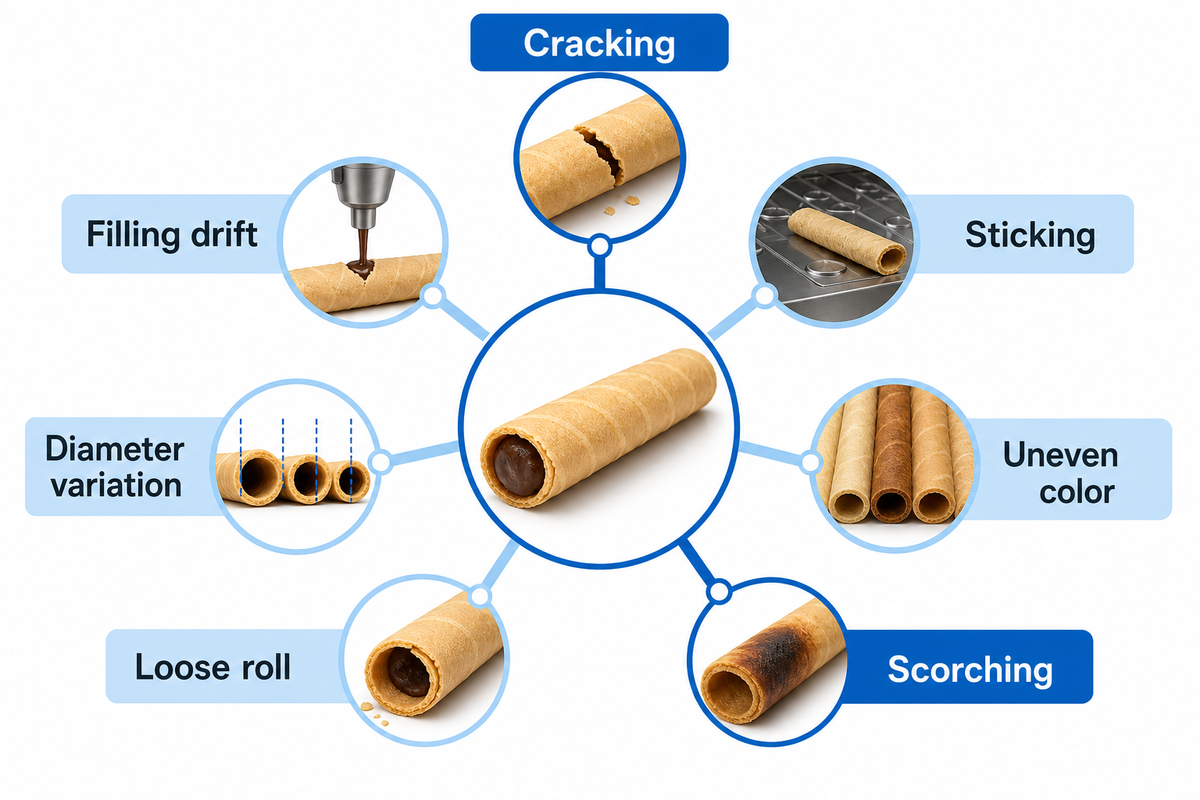
Each observation in this section is a symptom, not an explanation. The following controlled testing matrix indicates an area where testing can start. The matrix includes several variables because several independent studies suggest that formulation, heat distribution, surface state, thickness, and moisture can exhibit interactive effects.
| Symptom | Check first | Then isolate | Record |
|---|---|---|---|
| Cracking | Release-to-roll delay and sheet thickness | Dwell, formulation, cooling exposure | Cracks by station and elapsed time |
| Sticking | Surface cleanliness and release timing | Formulation, wear, thermal distribution | Plate position and take-off behavior |
| Uneven color | Zone readings and surface condition | Thickness, deposit, dwell | Color by plate or lane |
| Scorching | Dwell and local heat | Deposit mass and stop recovery | Defects before and after interruptions |
| Loose roll | Roll timing and tool geometry | Sheet flexibility and core position | Diameter and seam after cooling |
| Filling drift | Depositor timing and dose | Sheet arrival and viscosity | Core position in a cut sample |
| Diameter variation | Deposit mass, thickness, and tool position | Feed pulsing and roll pressure | Diameter sequence by time |
What are common egg-roll mistakes?
Changing multiple controls at once is the major mistake. Should an operator increase temperature, decrease the line speed, change batter type, and increase roll pressure, the next sample may improve but the reason is a mystery. If you want to define the defect in measurable terms, hold constant all of the requirements, change only one parameter, and test for what you believe to be a properly processed sample. A forming machine trial should record the isolated change and observed defect.
See if the defect occurs within a single plate, lane, disruption, batch, or operating interval. Then wait the agreed upon time to determine the crispness. The result becomes an established methodology, a repeatable test, rather than an educated guess.
Hygiene, Guarding, and Maintenance Access
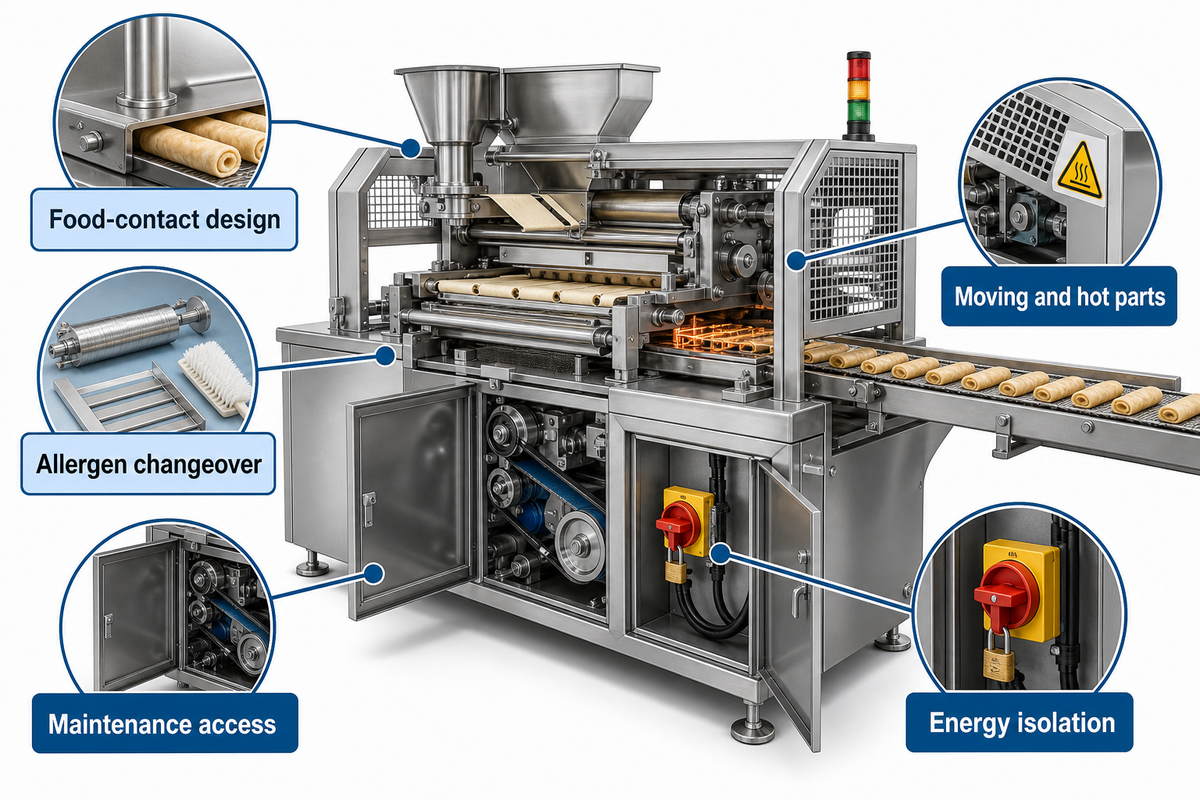
Stainless steel, although marketing language, isn’t a hygiene or safety file. Buyers need to see which surfaces contact food, how residues leave the machine, how operators reach inspection points, which hazards are guarded, and how energy is isolated before cleaning or service.
| Risk area | Evidence to request | Why the distinction matters |
|---|---|---|
| Food-contact design | Contact-surface list, material declarations, drainage and cleaning route | Cleanable construction is broader than material grade |
| Allergen changeover | Residue-control procedure, verification method, ingredient and label reconciliation | Egg, wheat, milk, nuts, or filling recipes can change the control plan |
| Moving and hot parts | Guard drawings, interlock function, access sequence, hot-surface controls | Guarding and thermal exposure are separate hazards |
| Servicing and unjamming | Electrical, mechanical, pneumatic, gas, and thermal energy-isolation points | A stopped control screen does not prove stored energy is controlled |
| Maintenance access | Lubrication map, removable parts, inspection intervals, spare-parts list | Poor access increases downtime and sanitation risk |
For U.S. facilities and activities within the purview of Part 117, 21 CFR 117.40 requires food equipment to be designable for cleaning and specifies food-contact surfaces. Separately, 21 CFR 117.135 addresses preventive controls, which include the protection of allergen cross-contact and labeling of finished food. The applicability and exemptions for the facility need to be determined. Neither page certifies a UD model.
OSHA’s general machine-guarding rule addresses hazards such as points of operation, ingoing nip points, and rotating parts. Where a given operation falls within the scope of bakery machinery, 29 CFR 1910.263 may make machinery-specific provisions. However, the scope should be checked; it may not be assumed. OSHA’s hazardous-energy standard generally applies to servicing where workers may suffer injury due to unexpected energy startup or unexpected release of stored energy. It also contains a narrow exception for qualifying minor servicing performed during normal production when the work is routine, repetitive, integral, and protected by effective alternative measures. An emergency stop or control-screen stop isn’t an energy-isolating device, so the plant safety professional should classify each cleaning, adjusting, etc., task.
For certificate-specific planning, continue with UD’s guide to food safety certifications for snack machinery. Keep the distinction clear: a certificate, a regulatory duty, and a hygienically designed machine feature are three different forms of evidence.
Integration and Utility Requirements Around the Machine
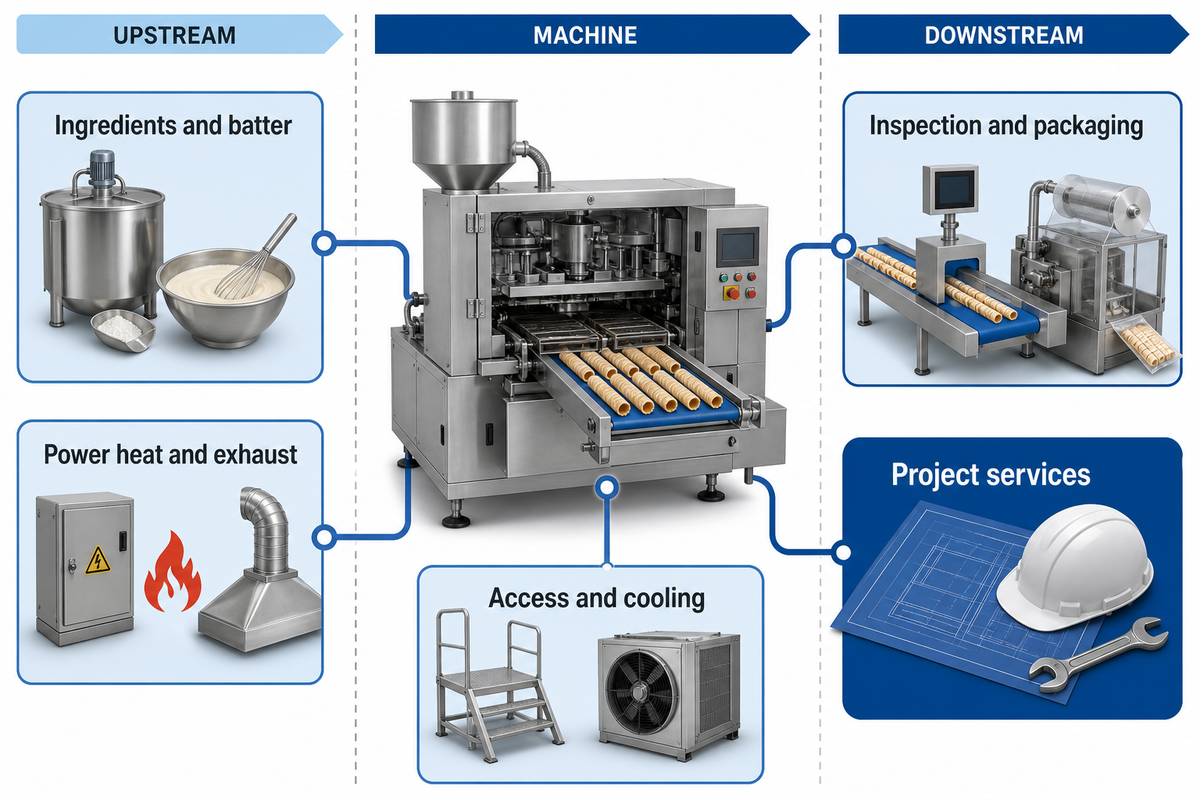
An accurate quotation for the main machine may still result in an incomplete project for the factory. Define the limit from the receipt of ingredients to the packaging of the product and allocate all interfaces to suppliers, buyers or third parties.
| Interface category | Interfaces to define | Typical decision owner |
|---|---|---|
| Dry ingredients | Charging, dust capture, housekeeping, allergen segregation | Safety and quality |
| Batter preparation | Mixing, holding, transfer, agitation, level control | Production and quality |
| Electrical supply | Voltage, frequency, connected load, isolation, controls | Engineering |
| Heating system | Fuel or electric heat, combustion air, exhaust, local code | Engineering and safety |
| Machine access | Guard clearance, cleaning route, service envelope, drainage | Safety, sanitation, maintenance |
| Cooling | Conveyor time, air conditions, humidity exposure | Production and quality |
| Inspection | Sampling, reject handling, count reconciliation | Quality |
| Packaging | Infeed rate, buffering, seal, coding, label control | Packaging and quality |
| Project services | Layout, freight, installation, commissioning, training, spares, acceptance | Procurement and project management |
Dry flour and other starch, sugar and powdered ingredients deserve a specific screening question. OSHA states that finely divided combustible material can become explosive when suspended air concentrations are at the right levels. This doesn’t mean every line with wet-batter has a combustible dust concern. Rather, it means that the upstream charging, extraction, housekeeping, ignition sources and material test data should be reviewed by qualified plant personnel where dry dust occurs.
Energy choice is also configuration-specific. Don’t copy voltage, gas consumption, exhaust, or cooling from another model. Match the quote to site utilities and local codes. UD’s guides on starting an egg roll production line and what a food production line includes provide the wider planning context.
A Buyer-Defined Witnessed-Run Evidence Pack
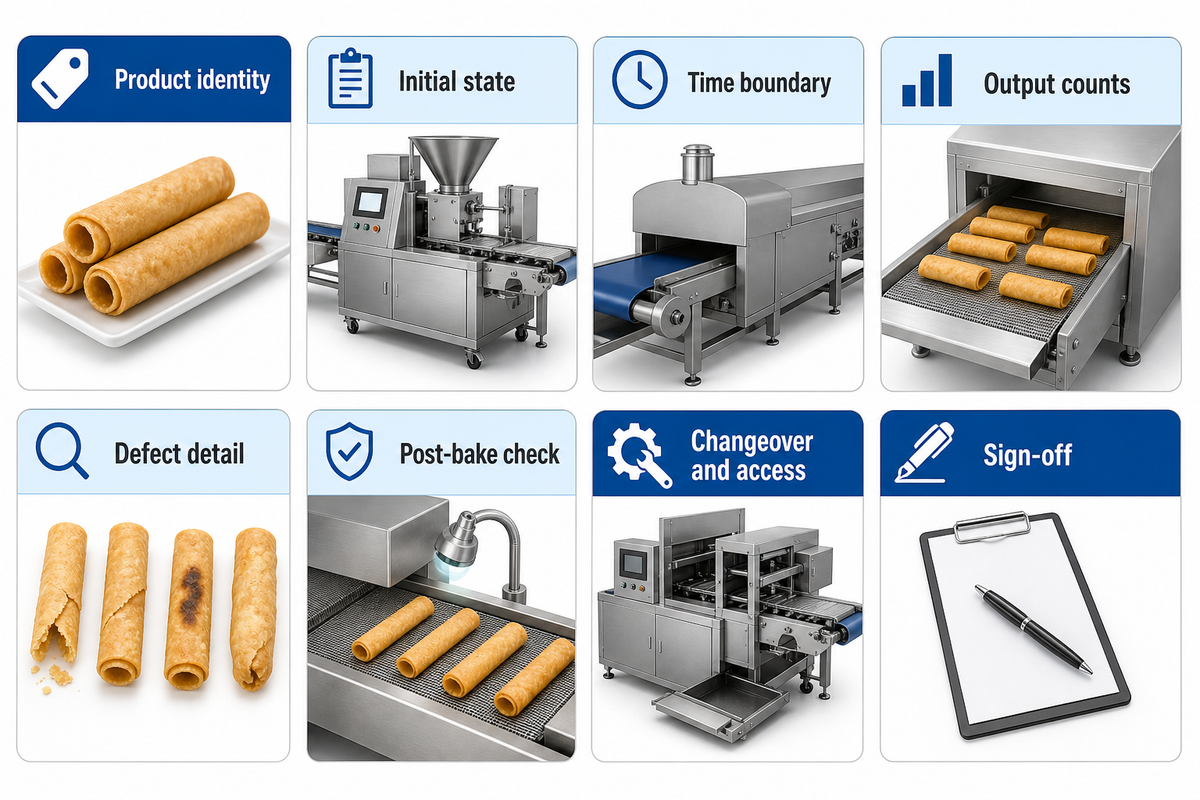
Demonstrations are most useful when given before the start button is pressed. The buyer and supplier agree which product will run, what condition the machine will be in for the start, how long the observation will be, which stops and defects will be counted, and who will sign the record. IEC 62381:2024 refers to acceptance of automation systems in the process industry. The focus of the publication is agreeing on responsibilities and procedures that will be implemented in response to the specified requirement. This article uses that agreement as a planning reference, and not as a certification for the egg roll machine. The BSI summary of packaging machine acceptance also refers to agreed upon test methods and time/output models.
Thirty minutes is an operable screening time, but this doesn’t equate to a factory-acceptance duration. Some sections specify tests: for instance, the Association of the Beverage Machinery Industry procedure takes an eight-hour test for main unit length, and for stand-alone units an eight-hour test comprising at least six hours of operation. This Association’s procedure doesn’t stipulate duration for an egg roll machine test. This illustrates that duration, downtime, counters, and scope must be explicit in the contract.
Be sure to define the sampling decision. The Acceptance Sampling Handbook of NIST describes a plan as (n, c): sample size and acceptance number. The number should be based on the risk of the buyer and the risk of the producer, so no arbitrary rejection percentage will be assigned. More important, a successful test run at one machine alone doesn’t validate lethality, sanitation, allergen control, or the control of storage. These require separate evidence. The following pack illustrates the limits of what a run can prove.
Witnessed-run evidence pack — agree these fields before testing
| Field | Record | Decision protected |
|---|---|---|
| Product identity | Recipe, batch, filling, dimensions, target texture | Prevents a substitute sample from proving the quote |
| Initial state | Cold start, warm start, warm-up duration, settings | Separates startup loss from steady operation |
| Time boundary | Clock start, clock stop, planned and unplanned stops | Makes availability auditable |
| Output counts | Total, first-pass accepted, rework, scrap | Separates cycles from released-good output |
| Defect detail | Cracks, sticking, color, diameter, seam, filling position | Shows which station needs correction |
| Post-bake check | Cooling time, room conditions, packaged or unpackaged test | Prevents discharge appearance from substituting for final texture |
| Changeover and access | Tool change, cleaning route, isolation points, restart | Exposes labor, downtime, and safety assumptions |
| Sign-off | Open items, owners, correction due date, retest rule | Turns a demonstration into a procurement record |
If the agreed-upon conditions don’t permit the intended recipe to run, don’t deem the speed stated in the brochure a verified output. Even if the screening run is successful, site acceptance, or factory acceptance, may not be accomplished. A clean sample doesn’t confirm sanitation, allergen control, lethality, or control of storage. Each open issue must be related to a drawing, record, hazard control, corrective action, or retest, not an informal verbal statement.
Turn the mechanism into a testable machine request
For a commercial egg roll project in the food industry, send UD Machine your sample, recipe or batter description, target dimensions, filling requirement, output goal, utilities, installation location, and witnessed-run conditions; list customization, technical support, and turnkey scope separately. The technical team would then be able to develop a configuration and a proof rather than provide a quote based on one speed.
Frequently Asked Questions
How much does an egg-roll machine cost?
Price depends on the machine class, output target, heat source, filling system, tooling, downstream scope, destination requirements, installation, and acceptance testing. Compare quotations using the same product specification and calculate cost per 1,000 accepted pieces. Low equipment price can become an expensive project if cooling, exhaust, guarding, change parts, or commissioning are outside the quoted boundary. Ask every bidder to identify exclusions, spare-parts assumptions, service travel, software backup, and the product used to establish the quoted rate. Include the cost of product trials, freight, utility work, operator time, planned wear parts, and any retest triggered by an unmet acceptance criterion. Then compare the expected good output and project boundary, not merely the purchase price.
Are egg-roll machines easy to use?
Routine operation becomes straightforward after the recipe, warm-up state, dosing, inspection method, and cleaning procedure are set. Operators still need training to recognize drift, respond to alarms, and isolate energy safely. A good handover also covers controlled restarts, defect sampling, sanitation checks, approved parameter ranges, and the point at which an operator should call maintenance or quality staff.
Is after-sales support available for industrial egg roll machinery?
Support scope varies by supplier and contract. Ask who handles installation guidance, commissioning, operator training, remote troubleshooting, spare parts, software backups, warranty response, and on-site service in your region. Put response times, included work, chargeable work, and language coverage in the quotation instead of relying on the phrase “after-sales support.”
Can one machine make filled and unfilled wafer rolls?
Some platforms offer optional filling equipment or change parts, but the answer is model- and product-specific. Filling changes deposit timing, core position, leakage control, sanitation, and sometimes cooling. Give the supplier both samples and ask for a witnessed changeover before assuming the same configuration can release both products at the quoted output.
What services should be defined when purchasing food machinery?
Define application review, layout and utility confirmation, sample trials, documentation, freight responsibilities, installation, commissioning, training, spare parts, warranty, software backup, remote support, factory acceptance, site acceptance, and corrective-action ownership. The important point is not how many services appear in a brochure. It is whether each service has a deliverable, responsible party, schedule, cost, and acceptance rule.
Method and commercial disclosure
UD Company was established in 2003. This document distinguishes first-party UD product information from independent research, official U.S. regulations, standard catalog summaries, and old patent prior art. Model figures aren’t general examples of performance. Purchasing links direct you to the UD Machine site. The final machine, food safety, and workplace safety requirements are irrevocably dependent on product, destination, facility, and contract review.
References & Sources
- Applied Sciences: wafer-baking plate thermal distribution, thickness, and color study
- Food Science & Nutrition: formulation effects on waffle sticking and release
- Low-moisture food study: Moisture content and water activity in wafers
- 21 CFR 117.40, Equipment and utensils
- 21 CFR 117.135, Preventive controls
- OSHA 1910.212, General machine guarding
- OSHA interpretation, Machine guarding for food processing
- OSHA 1910.147, Control of hazardous energy
- OSHA 1910.263, Bakery equipment
- OSHA, Combustible dust overview
- ISO 14159:2002, Hygiene requirements for machinery
- EHEDG GL 8, Hygienic Design Principles
- OEE Factors, availability, performance, and quality definitions
- Hygienic design of food equipment, cross-industry review
- NIST/SEMATECH, single acceptance sampling plans
- Association of the Beverage Machinery Industry, sector-specific acceptance procedure
- IEC 62381:2024, Factory and site acceptance testing
- US6254916B1, edible wafer-roll method and device
- US3633517A, prepared-sheet automatic egg-roll machine